U-Bend, Serpentine & Custom Bent Finned Tubes
Precision-engineered bent finned tubes manufactured to your exact geometry specifications. From standard U-bends to complex multi-plane serpentine configurations, every tube is custom-fabricated with precise bend radii, controlled wall thinning, and maintained fin integrity throughout the curved sections.
U-Bend (180°)
Standard return bendSerpentine (S-Shape)
Multi-pass continuous coilHairpin
Long-leg return elementJ-Bend / L-Bend
Single-end returnCustom Geometry
Compound & 3D bendsBending Process & Shape Configurations
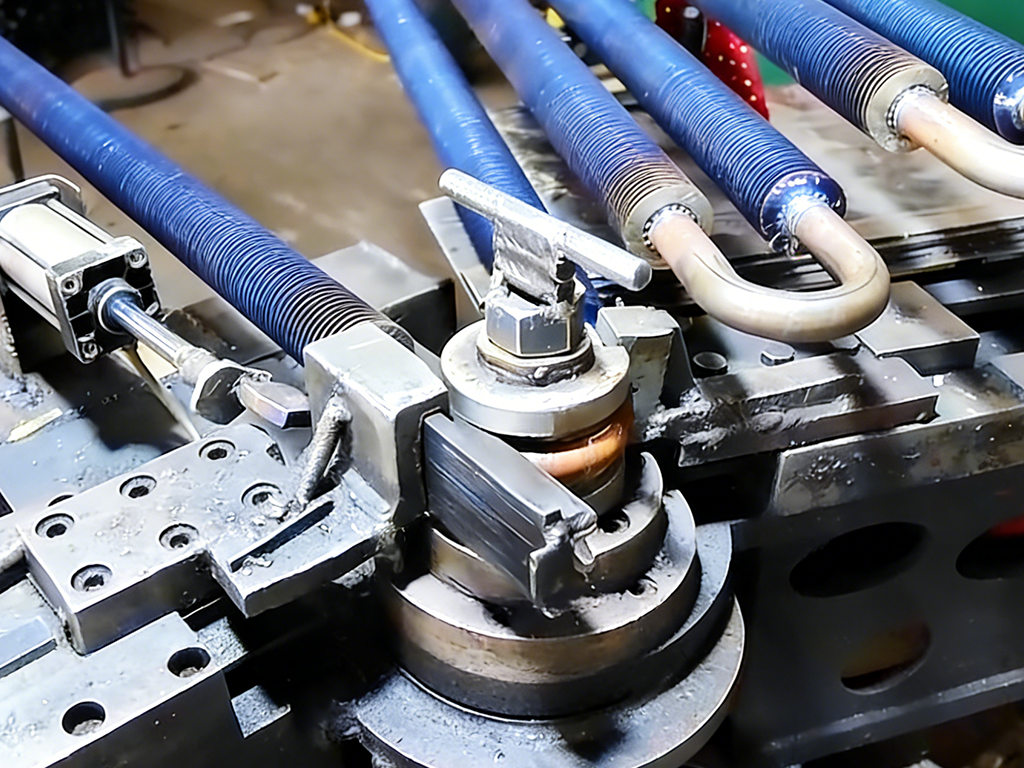
Precision Tube Bending — Process Overview
Our finned tube bending process uses CNC-controlled rotary draw bending machines with precision mandrels to ensure uniform bend geometry while preserving fin integrity. Each tube is bent to exact specifications after the finning process, maintaining the thermal performance characteristics of the straight sections through every curve.
The key to quality bent finned tubes lies in controlled bend radius, minimal wall thinning, and fin protection during the bending operation. Our tooling is custom-designed for finned tubes to prevent fin damage, crimping, or deformation in the bend zone.
U-Bend (180° Return)
Standard configuration for U-tube heat exchanger bundles. Bend radius 1.5D–3.0D.
Serpentine (S-Shape)
Continuous multi-pass coil with alternating 180° bends. 2–12+ passes.
Hairpin (Long Leg)
Single U-bend with extended straight legs. Common in double-pipe exchangers.
J-Bend / L-Bend
Single-end return with one straight leg. For compact header arrangements.
Manufacturing Process Options — Finning Before or After Bending
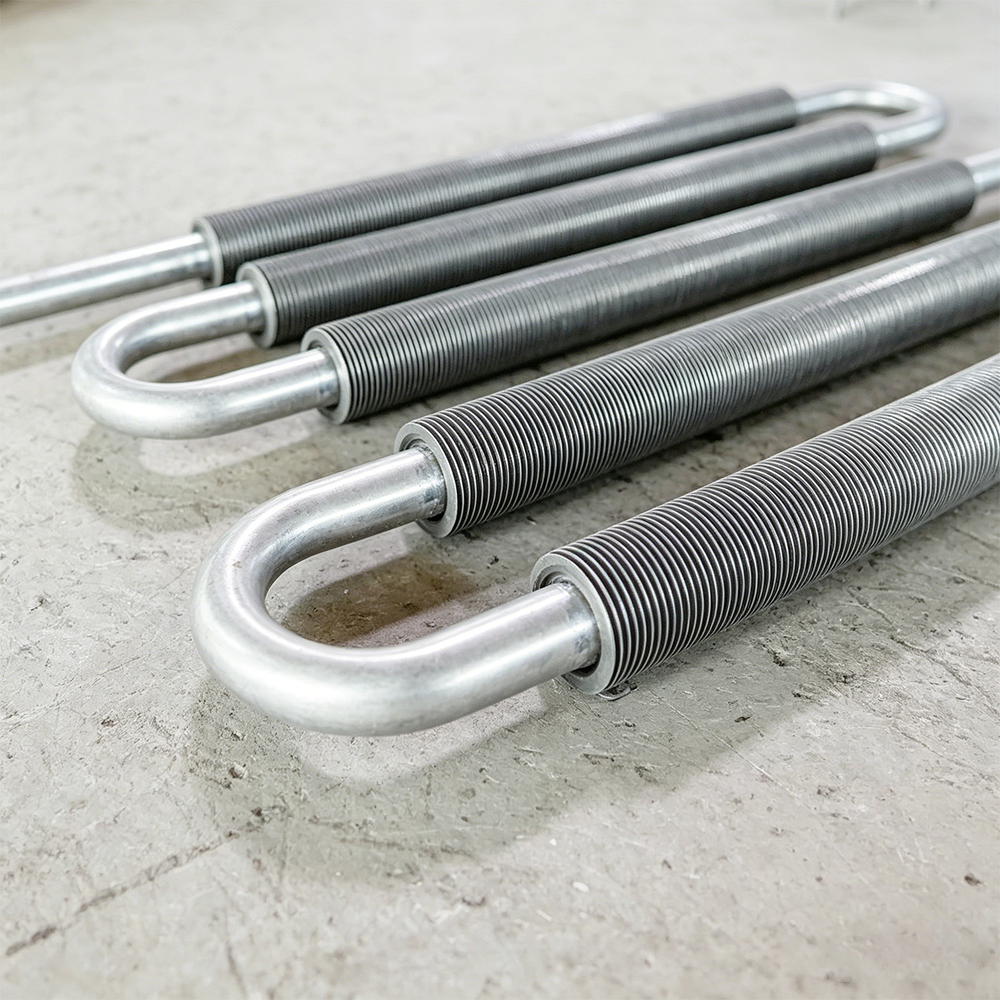
Two Process Routes — Choose Based on Your Design
We offer two distinct manufacturing routes for bent finned tubes, each optimized for different application requirements. The choice of process route depends on bend complexity, fin type, and whether fins are required in the bend zone.
| Route A: Fin-First, Then Bend | The tube is fully finned on the straight, then bent to shape. Fins remain in the bend zone with controlled spacing. Most common and cost-effective route for standard U-bends and serpentine coils. |
| Best For | U-bend bundles, serpentine coils, hairpin elements, standard radii ≥ 1.5D |
| Fin Types Supported | High-frequency welded, laser welded, spiral wound, extruded |
| Bend Zone Fins | Present — fin spacing may open slightly on outer radius, acceptable for most applications |
| Route B: Bend First, Then Fin | The bare tube is bent to shape first, then finned on the straight sections only. Bend zones remain bare. Used when tight radii or fin-free bend areas are required. |
| Best For | Tight radii < 1.5D, thick fins, complex multi-plane bends, J-bends, expansion loops |
| Fin Types Supported | High-frequency welded, laser welded, embedded |
| Bend Zone Fins | Absent — straight sections only are finned, bend remains bare for header access or clearance |
Material Options — Tube & Fin Combinations for Bent Configurations
All materials available for straight finned tubes can be supplied in bent configurations. The table below highlights material combinations commonly specified for U-bend, serpentine, and custom bent finned tubes. Bendability is assessed during the engineering review phase based on material, wall thickness, and bend radius.
| Tube Material | Fin Material | Fin Type | Min Bend Radius | Bendability | Typical Bent Configuration | Common Applications |
|---|---|---|---|---|---|---|
| ▸ Carbon Steel Bent Finned Tubes | ||||||
| Carbon Steel (A179 / A192) | Carbon Steel | HF Welded / Laser Welded | 1.5D | ★★★★★ Excellent | U-Bend, Serpentine, Hairpin | Boiler economizers, flue gas coolers, HRSG bundles |
| Carbon Steel (A210 Gr.A1/C) | Carbon Steel | HF Welded | 2.0D | ★★★★☆ Very Good | U-Bend, Hairpin | Large utility boiler economizers, process heaters |
| Carbon Steel (A179) | Galvanized Steel | HF Welded | 2.0D | ★★★★☆ Very Good | U-Bend, Serpentine | Outdoor air-cooled coils, cooling tower bypass |
| ▸ Stainless Steel Bent Finned Tubes | ||||||
| SS304 / SS304L | SS304 / SS304L | HF Welded / Laser Welded | 1.5D | ★★★★★ Excellent | U-Bend, Serpentine, J-Bend | Food processing, chemical HX, pharmaceutical coils |
| SS316 / SS316L | SS316 / SS316L | Laser Welded | 1.5D | ★★★★★ Excellent | U-Bend, Serpentine, Custom | Marine exchangers, offshore, desalination, chemical plants |
| SS321 / SS347 | SS321 / SS347 | Laser Welded | 2.0D | ★★★★☆ Very Good | U-Bend, Hairpin | High-temp heat recovery, furnace recuperators |
| ▸ Copper & Copper Alloy Bent Finned Tubes | ||||||
| Copper (C12200 / C11000) | Copper | Extruded / HF Welded | 1.2D | ★★★★★ Superior | U-Bend, Serpentine, Hairpin, Custom | HVAC coils, heat pumps, data center cooling, refrigeration |
| Copper (C12200) | Aluminum | HF Welded / Embedded | 1.5D | ★★★★★ Excellent | U-Bend, Serpentine | Air-cooled condensers, generator set radiators |
| Cu-Ni 90/10 (C70600) | Copper / Cu-Ni | Laser Welded | 2.0D | ★★★★☆ Very Good | U-Bend, Hairpin | Shipboard condensers, seawater cooling, desalination |
| ▸ Alloy Steel & Specialty Bent Finned Tubes | ||||||
| T11 / T22 (Cr-Mo) | Carbon Steel / T11 | HF Welded | 2.5D | ★★★☆☆ Good | U-Bend, Hairpin | Refinery heaters, high-temp petrochemical furnaces |
| Duplex SS (2205 / 2507) | Duplex SS / SS316L | Laser Welded | 2.5D | ★★★☆☆ Good | U-Bend, Custom | Offshore platforms, aggressive chemical environments |
| ▸ Bending Capability Summary | ||||||
| Minimum Bend Radius | 1.2D (copper) / 1.5D (CS & SS) / 2.0D (alloy) | Smaller radii available with bend-first-then-fin process | ||||
| Bend Angle Range | 15° – 180° (any specified angle) | Multi-plane compound bends available | ||||
| Tube OD Range for Bending | 9.5mm – 50.8mm (3/8″ – 2″) | Larger diameters require engineering review | ||||
| Max Tube Length After Bending | Leg length up to 9m per side | Dependent on tube diameter and handling equipment | ||||
Application Range & Industry Sectors
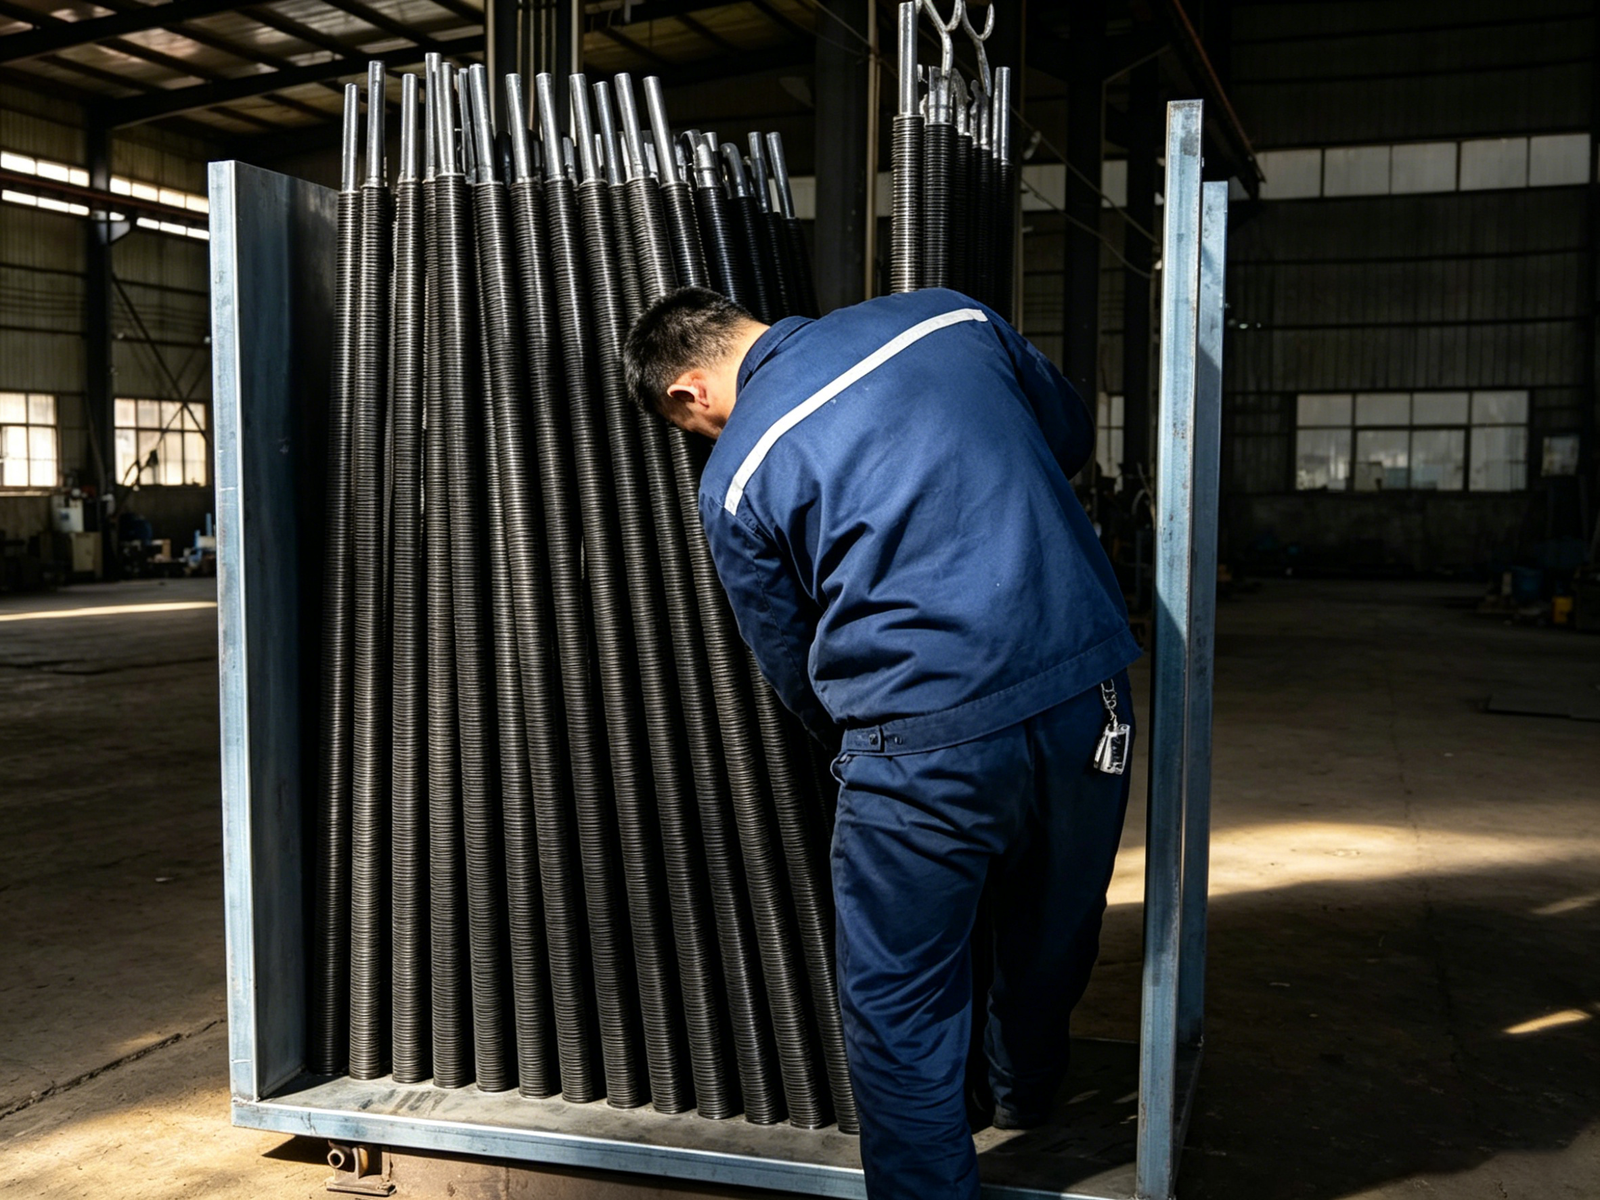
Shell & Tube Heat Exchanger Bundles
U-bend finned tubes are the core heat transfer element in U-tube shell and tube heat exchangers. The U-bend configuration allows free thermal expansion of the tube bundle without expansion joints, making it ideal for applications with significant temperature differences between shell and tube sides.
- U-Tube Bundles (BEU Type): Multi-row nested U-bend finned tubes with progressive bend radii form compact, high-density heat exchanger bundles for oil cooling, steam heating, and process applications.
- Floating Head Bundles (BES/BEP): Straight finned tubes with single-end U-bends allow complete bundle removal for mechanical cleaning of both shell and tube sides.
- Kettle Reboiler Bundles (BKU): Hairpin and U-bend finned tubes in kettle shells for boiling and vaporization service in chemical and petrochemical plants.