High-Frequency Welded Finned Tubes
Industry-standard high-frequency welded finned tubes offering the optimal balance of cost-effectiveness, production speed, and reliable thermal performance. The most widely specified finned tube type for general industrial heat transfer applications worldwide.
High-Frequency Welding Technology
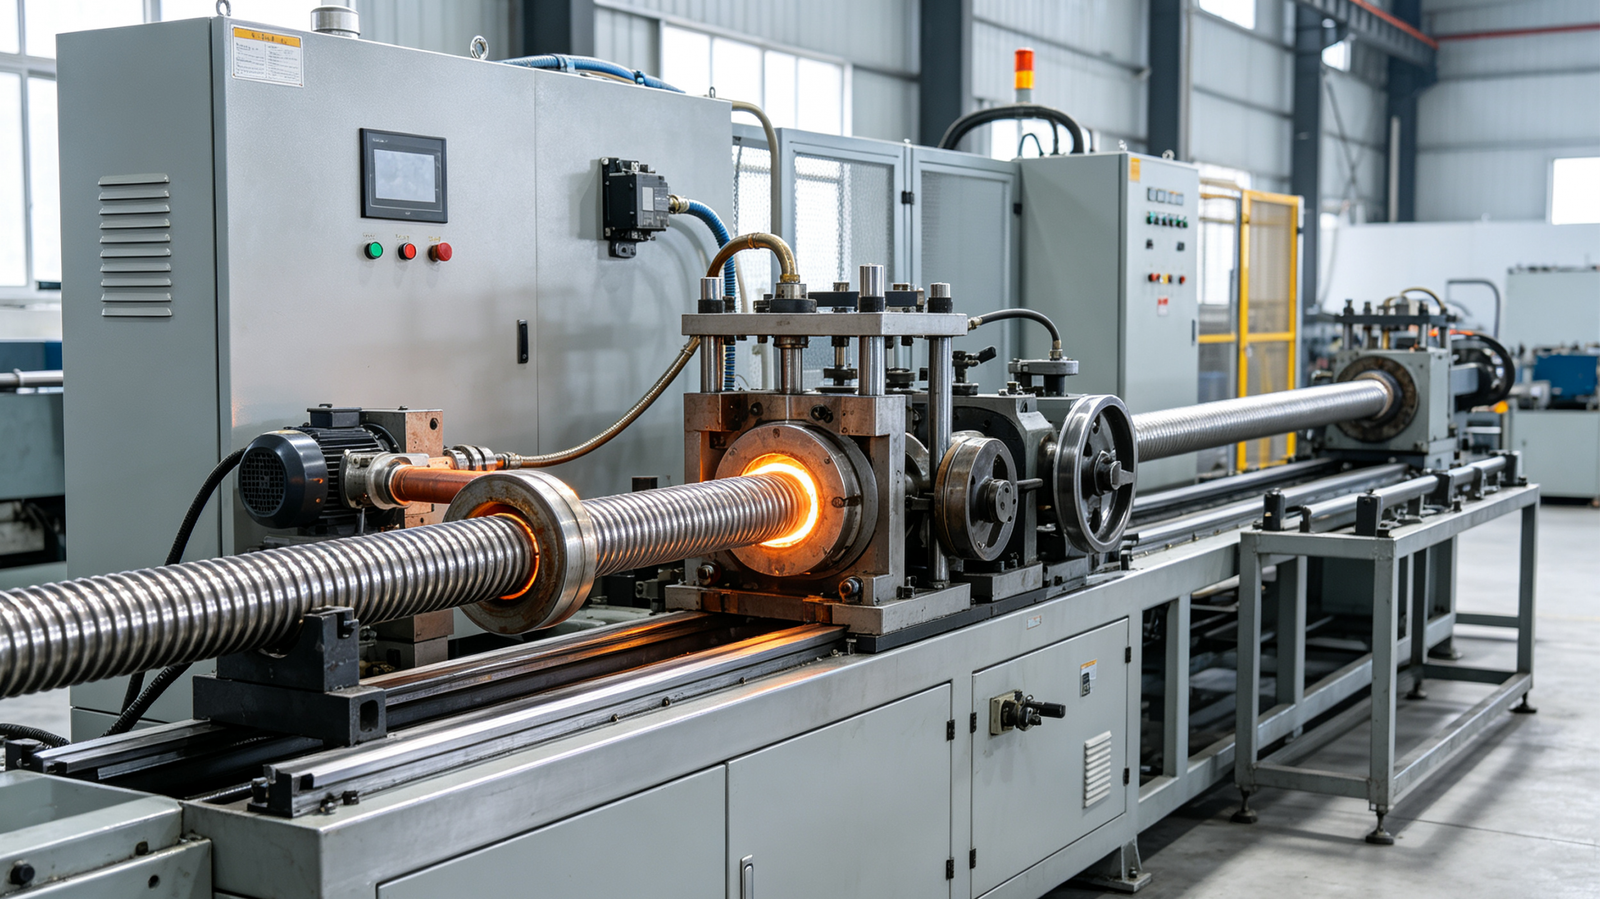
How High-Frequency Welding Works
High-frequency welding uses electromagnetic induction to generate concentrated heat at the interface between the fin base and the tube surface. A high-frequency electric current (typically 200–500 kHz) passes through an induction coil, creating rapid localized heating that brings the contact surfaces to welding temperature within milliseconds.
As the tube rotates and advances through the welding station, the fin strip is continuously fed and pressed against the heated tube surface. The combination of pressure and localized melting creates a continuous, uniform weld bead along the entire fin helix — all at production speeds exceeding 50 meters per minute.
- Induction Heating Principle: A water-cooled induction coil surrounds the tube, generating eddy currents that heat the tube surface and fin base precisely at the weld point without direct electrical contact.
- Continuous Helical Welding: The fin strip is wound around the rotating tube in a continuous spiral, with the weld formed progressively along the helix path — ideal for long production runs.
- Pressure-Forge Bonding: Pneumatic or hydraulic pressure rollers press the heated fin base firmly against the tube, creating a forged metallurgical bond with excellent mechanical strength.
- Rapid Cooling: The localized heat dissipates quickly after the weld point passes, creating a fine-grained microstructure in the weld zone with minimal distortion to the tube body.
Advantages & Process Comparison
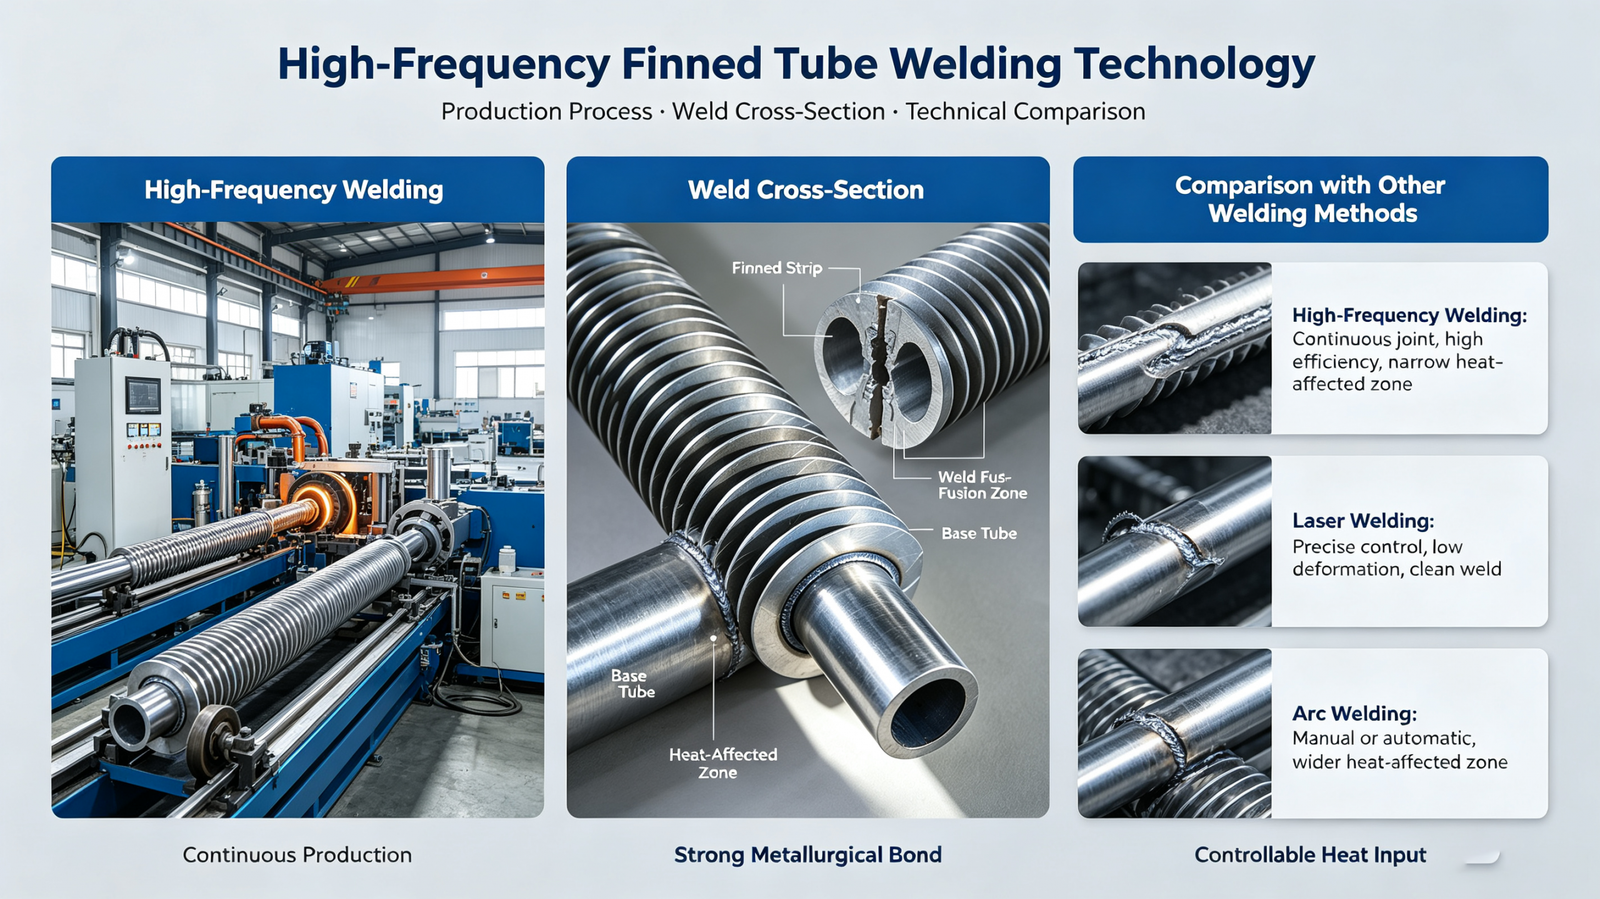
Why Choose High-Frequency Welded Finned Tubes
High-frequency welding remains the dominant production method for industrial finned tubes due to its unmatched combination of speed, cost-effectiveness, and proven reliability across decades of field service in millions of heat exchangers worldwide.
| Production Speed | 50–80 m/min — fastest among all fin welding methods |
| Weld Strength | ≥80% of base fin material tensile strength |
| Material Range | Carbon steel, low-alloy steel, stainless steel (ferritic/austenitic) |
| Fin Thickness Range | 0.8mm – 2.5mm standard |
| Fin Height Range | 6mm – 25mm |
| Cost Efficiency | Lowest cost per meter for qualified materials |
- Proven Track Record: Established technology with over 50 years of industrial application history and extensive performance data.
- Excellent for Carbon Steel: The preferred method for carbon steel finned tubes used in boilers, economizers, and flue gas heat recovery applications.
- Continuous Long Lengths: Single tubes up to 15 meters can be continuously finned without intermediate joints.
Material Options — Tube & Fin Combinations
High-frequency welding is compatible with a broad range of ferrous materials. The table below details standard and extended material combinations available for our high-frequency welded finned tubes. Custom diameter and material requests are welcomed for volume orders.
| Tube Material | Fin Material | Tube OD Range | Fin Height Range | Max Temp | Typical Applications |
|---|---|---|---|---|---|
| ▸ Carbon Steel Combinations (Most Common) | |||||
| Carbon Steel (A179 / A192) | Carbon Steel | 19.0mm – 51.0mm | 8mm – 20mm | 450°C | Boilers, economizers, flue gas coolers, waste heat recovery |
| Carbon Steel (A210 Gr.A1 / C) | Carbon Steel | 25.4mm – 76.2mm | 10mm – 25mm | 500°C | Power plant HRSG, large economizers, process heaters |
| Carbon Steel (A179) | Galvanized Steel | 19.0mm – 38.1mm | 8mm – 16mm | 350°C | Atmospheric corrosion resistance, outdoor air-cooled exchangers |
| ▸ Low-Alloy Steel Combinations | |||||
| T11 / T22 (1.25Cr-0.5Mo / 2.25Cr-1Mo) | Carbon Steel / T11 | 25.4mm – 50.8mm | 10mm – 19mm | 550°C | High-temperature refinery heaters, petrochemical furnaces |
| T91 (9Cr-1Mo) | T91 / SS409 | 31.8mm – 50.8mm | 10mm – 19mm | 600°C | Supercritical boilers, advanced heat recovery systems |
| ▸ Stainless Steel Combinations | |||||
| SS304 / SS304L | SS304 / SS304L | 15.9mm – 50.8mm | 6mm – 19mm | 550°C | Food processing, chemical plants, pharmaceutical equipment |
| SS316 / SS316L | SS316 / SS316L | 15.9mm – 50.8mm | 6mm – 19mm | 550°C | Marine heat exchangers, offshore, chemical processing |
| SS321 / SS347 | SS321 / SS347 | 19.0mm – 38.1mm | 8mm – 16mm | 600°C | High-temperature corrosive environments, furnace recuperators |
| SS409 / SS410 | SS409 / SS410 | 19.0mm – 50.8mm | 8mm – 19mm | 450°C | Economical stainless option, moderate corrosion applications |
| ▸ Tube Size Availability | |||||
| Standard Tube OD Range | 15.9mm (5/8″) – 76.2mm (3″) | Larger diameters available upon engineering review | |||
| Standard Fin Height Range | 6mm – 25mm | Custom fin heights available per application requirements | |||
| Standard Fin Thickness Range | 0.8mm – 2.5mm | Thinner/thicker fins available upon request | |||
| Maximum Tube Length | Up to 15 meters | Longer lengths possible with intermediate supports | |||
High-frequency welding is optimized for ferrous materials. For non-ferrous materials such as copper, aluminum, or titanium, alternative welding methods (laser or TIG) are recommended. Contact our engineering team for material combination feasibility assessment.
Application Range & Industry Sectors
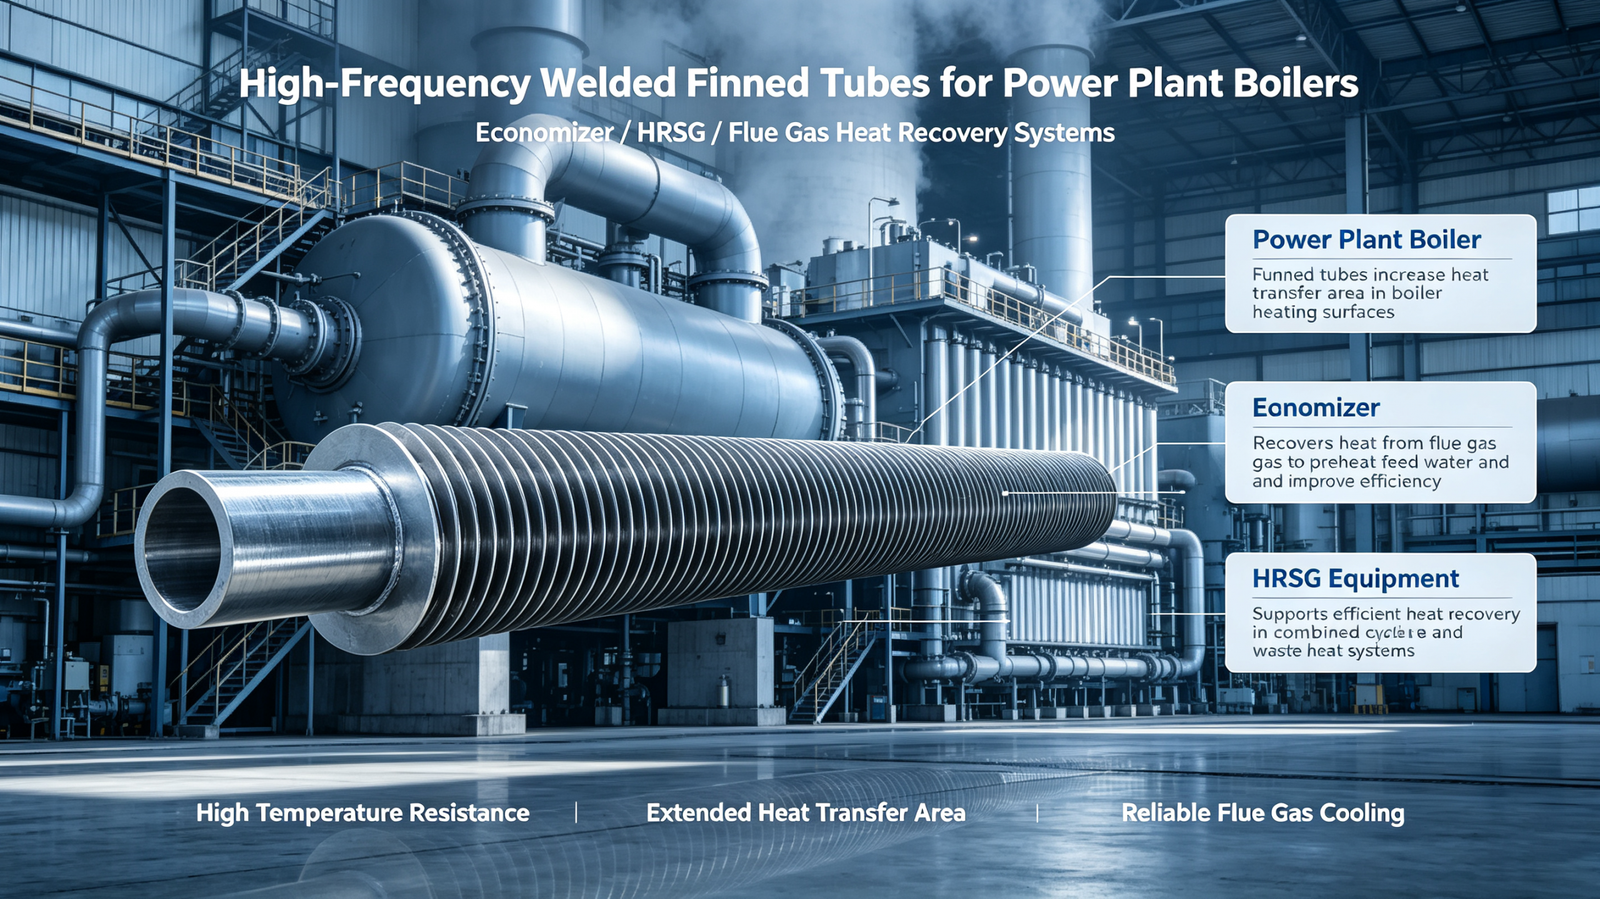
Power Generation & Boiler Systems
High-frequency welded finned tubes are the standard choice for boiler economizers and HRSG systems in power plants worldwide. The high-speed production process enables cost-effective manufacturing of the large tube quantities required for utility-scale projects.
- Economizers: Carbon steel finned tubes recover waste heat from boiler flue gas to preheat feedwater, improving overall plant efficiency by 5–10%.
- HRSG (Heat Recovery Steam Generators): Thousands of finned tubes per unit in combined cycle power plants, with HF welding enabling competitive pricing for bulk orders.
- Biomass & Waste-to-Energy Boilers: Robust carbon steel finned tubes handle the aggressive flue gas conditions from alternative fuel combustion.
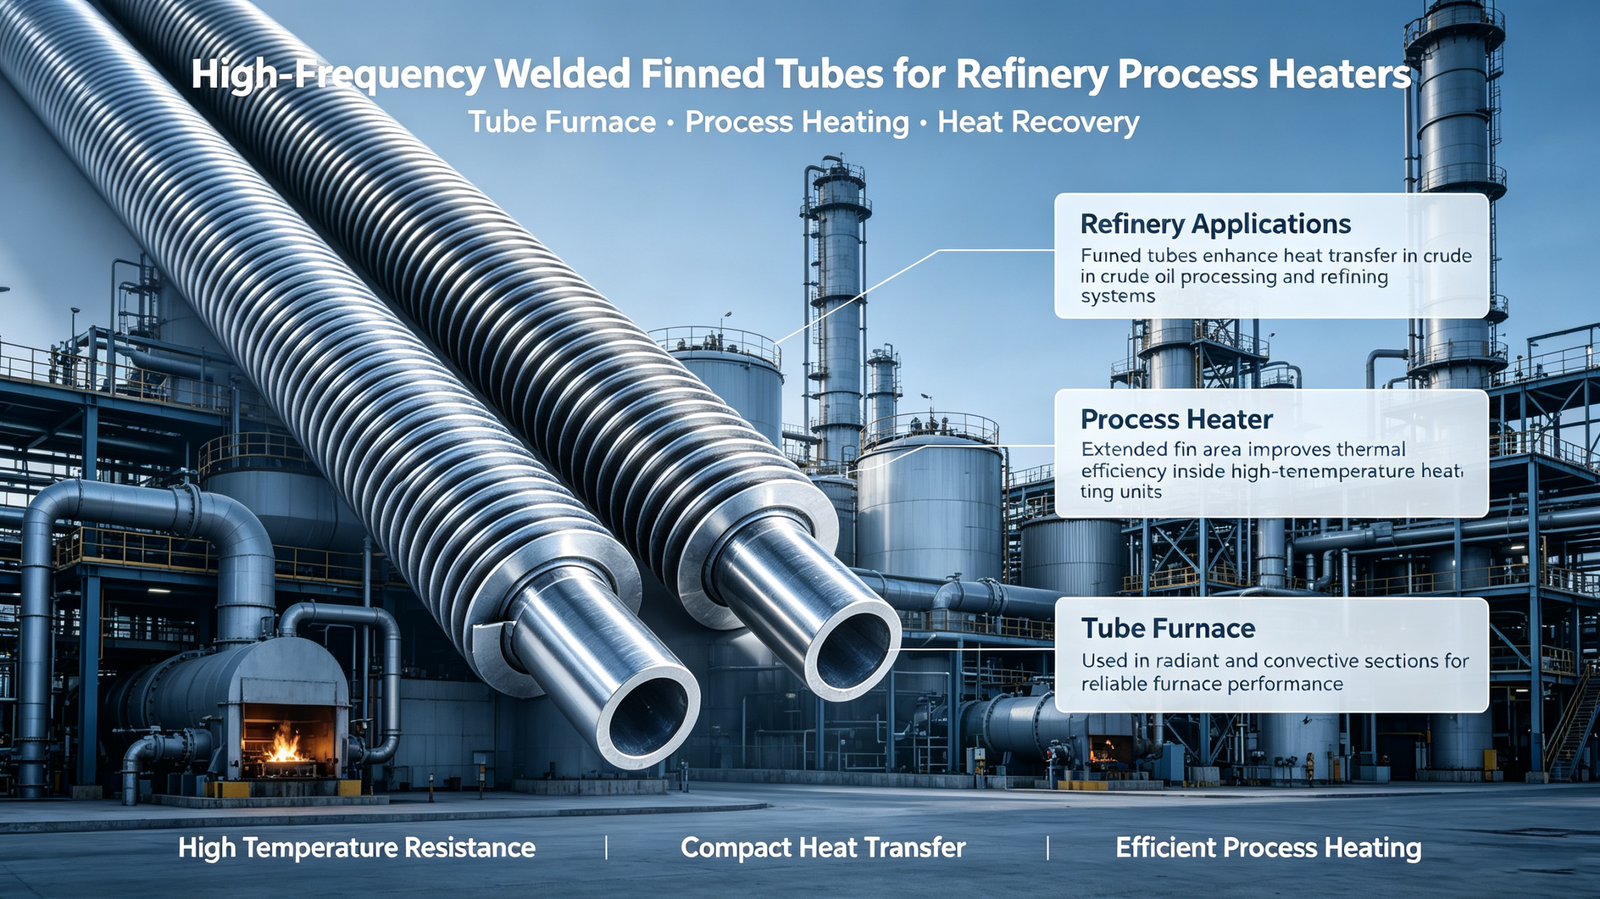
Petrochemical & Process Heating
In refineries and chemical plants, high-frequency welded finned tubes are extensively used in fired heaters, convection banks, and process heat exchangers where reliable performance under continuous high-temperature operation is mandatory.
- Fired Heater Convection Sections: Alloy steel finned tubes (T11/T22) for refinery crude heaters and hydrocracker furnaces operating at 500–600°C.
- Process Gas Coolers: Stainless steel finned tubes for cooling corrosive process gases in chemical production lines.
- Heat Recovery from Flue Gas: Carbon steel and stainless steel options for recovering thermal energy from combustion exhaust streams.
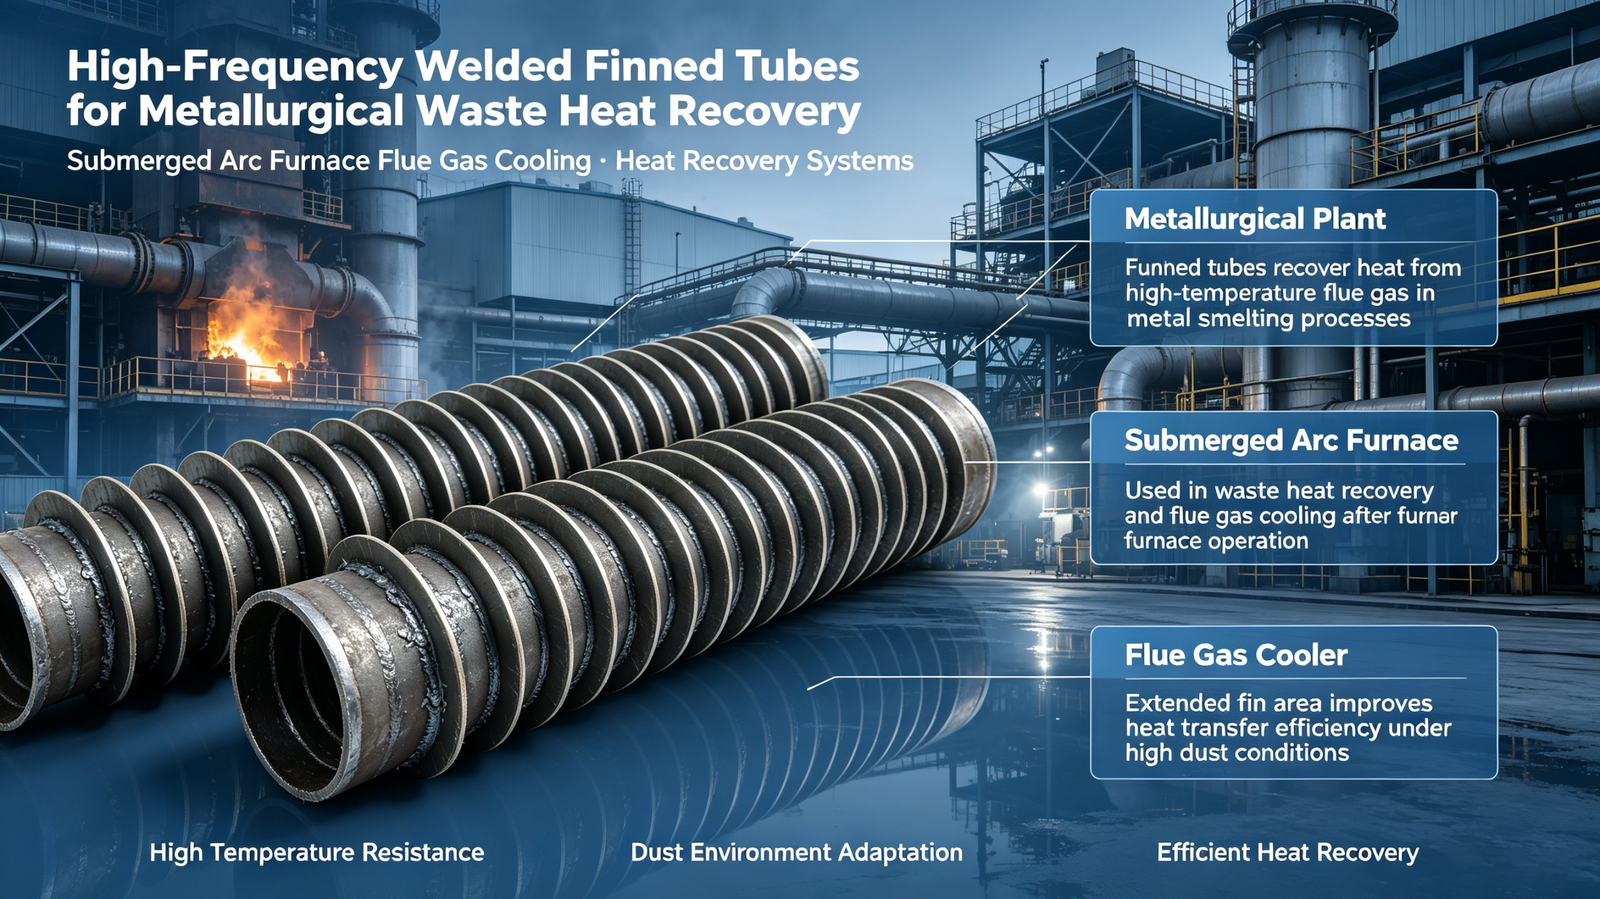
Metallurgy, Mining & Heavy Industry
The metallurgical and mining industries generate enormous quantities of high-temperature waste heat. High-frequency welded finned tubes provide the durable, cost-effective heat transfer surface needed for large-scale heat recovery systems in these demanding environments.
- Steel Mill Waste Heat Recovery: Carbon steel finned tubes in blast furnace and electric arc furnace off-gas cooling systems recovering heat for power generation or process use.
- Cement Plant Preheaters: Large-diameter finned tubes for cooling cement kiln exhaust gases and preheating combustion air.